Semiconductor test engineering is an essential part of manufacturing, especially as integrated circuit (IC) designs become more complex and time-to-market pressures increase. As more transistors continue to be fabricated on a single integrated circuit, it is necessary to ensure that the processing defect is not impaired. With global chip sales trending toward a $1 trillion market by 2030, the ability to maintain high yields through precise testing is the industry’s primary competitive advantage.
Test engineering plays a crucial role in the semiconductor industry, contributing to developing and producing high-quality semiconductor devices. Its primary focus is to ensure that semiconductor chips meet specified performance, reliability, and quality standards before they are shipped to customers.
Significance of Test Engineering in the Semiconductor Industry
In Test engineering, the functionality and performance of semiconductor devices are accessed through the development of test programs and methodologies. Test engineers design various tests and scripts to validate the chip features and functions. Modern test engineers are now utilizing AI-driven analytics to predict failures and optimize test time, effectively reducing the “cost of test,” which can account for up to 20% of a chip’s total manufacturing cost.
Extensive testing methodologies are used to identify and address defects, manufacturing variations, and other issues that potentially impact the chip’s performance. Test engineers select and maintain specialized test equipment, Automated Test Equipment (ATE), Oscilloscope, and other testing equipment. The rise of Chiplets and 3D IC stacking has introduced “Heterogeneous Testing,” requiring engineers to validate multi-die communication across a single interposer.
Test engineers conduct reliability tests, such as:
- ESD (ElectroStatic Discharge) & Latch-Up (LU): Testing protection against static shocks.
- TC (Temperature Cycling) & Thermal Aging: Assessing mechanical durability over time.
- Accelerated Life Testing: Simulating years of use in weeks to meet strict Automotive (AEC-Q100) and Industrial standards.
Latest Testing Equipment for Semiconductor
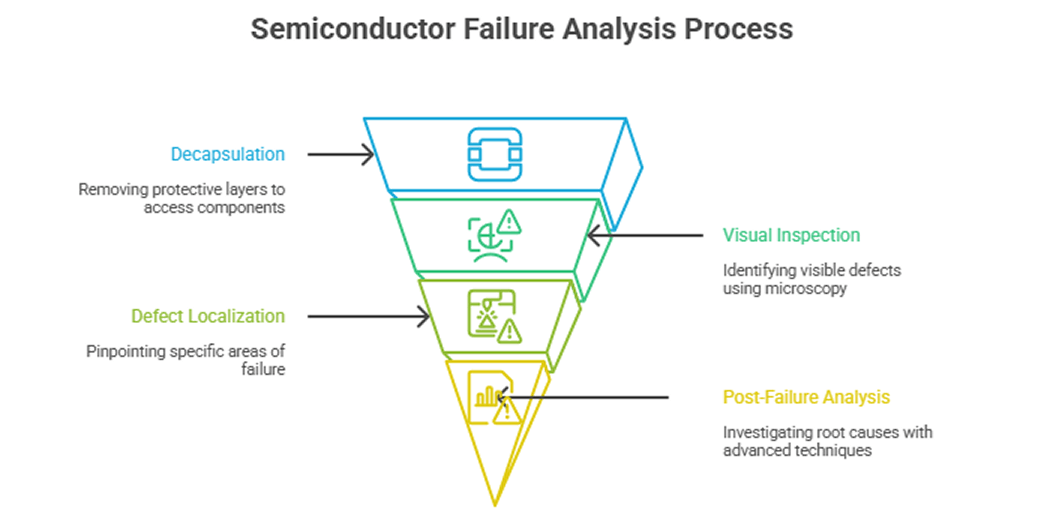
Decapsulation
It refers to removing the protective outer layers or encapsulation materials from a semiconductor device to access and analyze the internal components. This process is often necessary to understand the causes of semiconductor device defects, failures, or performance issues. Microwave-Induced Plasma (MIP) decapsulation has become the gold standard for “damage-free” removal, especially for sensitive 3D stacked dies.
Methods to perform decapsulation:-
Chemical Etching:
A standard method involving selective acids to dissolve encapsulation while leaving the silicon die intact.
Laser Decapsulation:
Laser ablation selectively removes material with high precision, minimizing the risk of “over-etching” the underlying bond wires.
Failure Analysis:
Decapsulation helps investigators determine whether a device failed due to internal defects, such as wire bond failures, delamination, or contamination.
Optical Microscopy:
Optical microscopy plays a significant role in semiconductor testing and analysis. It is a versatile tool that allows engineers and researchers to visually inspect semiconductor devices, evaluate their quality, and identify various issues and anomalies. Let’s see how it is used
Visual Inspection:
Optical microscopes are used for routine visual inspection of semiconductor wafers, packaged devices, and integrated circuits. Engineers and technicians can examine the devices for visible defects, such as cracks, scratches, contamination, or bond wire issues. Visual inspection is essential to quality control and process monitoring in semiconductor manufacturing.
Defect Localization:
When a semiconductor device fails or exhibits performance issues, optical microscopy can help localize and identify the specific area or component responsible for the problem. By zooming in on the device, analysts can pinpoint defects affecting device functionality, such as shorts, opens, or delaminations.
Wafer Mapping:
Optical microscopes can capture images of entire semiconductor wafers, allowing for wafer mapping and defect localization. This is crucial for identifying areas of concern and optimizing the manufacturing process.
Post-Failure Analysis:
After a semiconductor device has failed, optical microscopy can be used in conjunction with other techniques, such as scanning electron microscopy (SEM) or transmission electron microscopy (TEM), to investigate the root cause of the failure.
Do Test Packages Have Any Role to Play in Semiconductor Testing
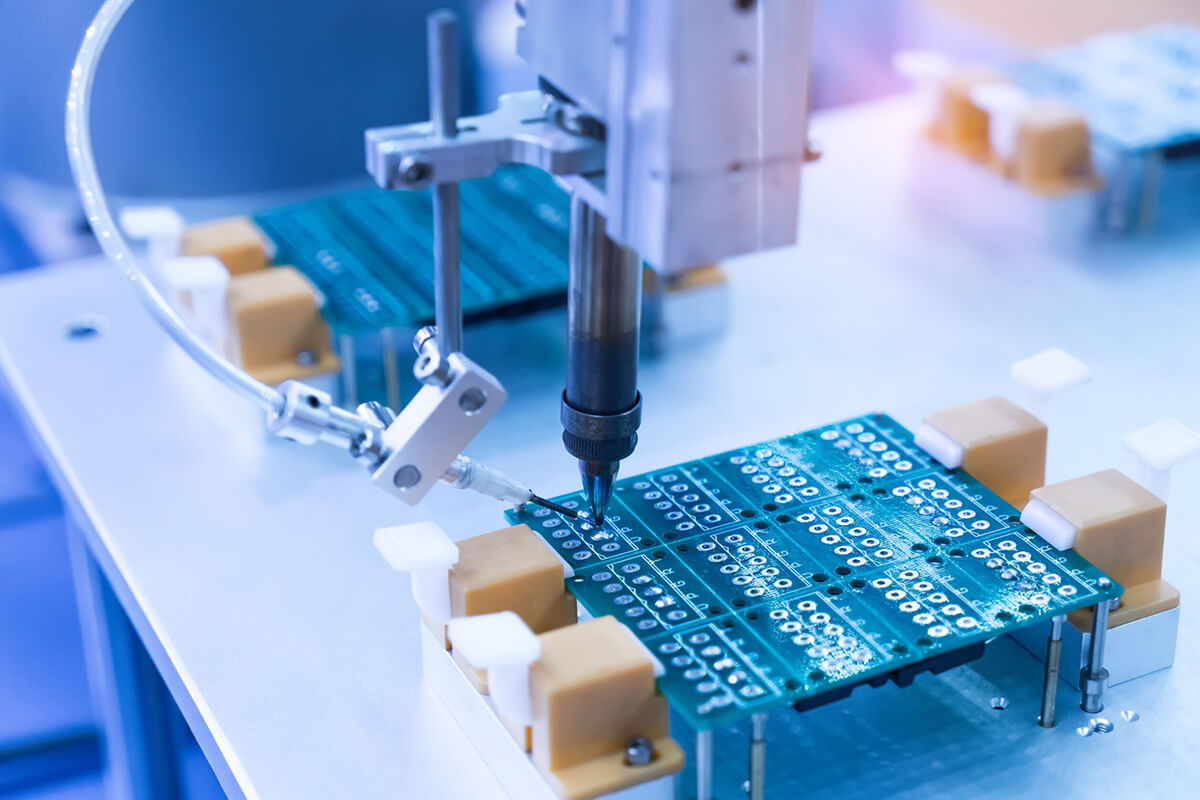
Test packages, also known as test fixtures or sockets, play a major role in test engineering and management semiconductor testing, especially for packaged integrated testing (ICs). These packages are designed to facilitate the electrical testing of semiconductor devices and ensure they function correctly. Below are the key points that illustrate the role of test packages in semiconductor testing.
Physical Protection:
Test packages serve as protective enclosures for semiconductor devices during test engineering. They shield the device from physical damage, electrostatic discharge (ESD), and contamination. This is especially critical because semiconductor devices are often sensitive to external factors.
Thermal Management:
Some semiconductor devices generate heat during testing, affecting their performance or reliability. Test packages may incorporate features for thermal management, such as heat sinks or cooling systems, to maintain the device’s temperature within acceptable limits.
Signal Integrity:
Maintaining signal integrity is crucial in semiconductor testing. Test packages are engineered to minimize signal losses, reflections, and noise, ensuring test signals accurately represent the device’s behavior.
Understanding the Difference: Hardware Design vs. PCB Design
Avail the Testing Proficiency Within a Robust Test Setup: Choose Tessolve
We are renowned for our Engineering Testing Services, helping semiconductor companies in IC Design, Test and Product Engineering, and Failure Analysis. Tessolve’s Characterization Lab is a unique facility equipped with AI-powered ATE platforms (Teradyne, Advantest) to perform complete Electrical Characterization of Silicon Devices.
We are a one-stop shop for companies looking for advanced OSAT/ATMP (Assembly, Test, Marking, and Packaging) solutions. With us, you can perform testing, debugging, and characterizing using advanced technologies cost-effectively and quickly.
Frequently Asked Questions
1. Why is “at-speed” testing critical for 5G and AI chips?
Many defects only appear at high operational frequencies; at-speed testing ensures the chip maintains signal integrity under peak workloads.
2. What is the benefit of Microwave-Induced Plasma (MIP) decapsulation?
It provides isotropic, chemical-free etching that preserves sensitive copper bond wires and 3D stacks better than traditional acid-based methods.
3. What is involved in IC semiconductor test services and product qualifications?
These services include functional validation, burn-in, and stress tests to ensure chips meet stringent performance and reliability standards.
4. What are the most common semiconductor device testing techniques?
Key techniques include DC/AC parametric testing, functional examination, and structural tests like scan-based logic and memory BIST validation.
5. What are the basic testing methods used in semiconductor manufacturing?
Manufacturing involves wafer-level probing to identify bad dies early and final package testing to verify finished product functionality.